
Why do solenoid valves that test perfectly in the laboratory frequently jam or act sluggishly after going online? Many engineers new to fluid control often assume that a solenoid valve will open as long as it is energized and close when de-energized. This oversimplified understanding is often the root cause of frequent subsequent system failures.
Solenoid Valve Principles and Common Misconceptions: Why Energization Does Not Equal Instant Action
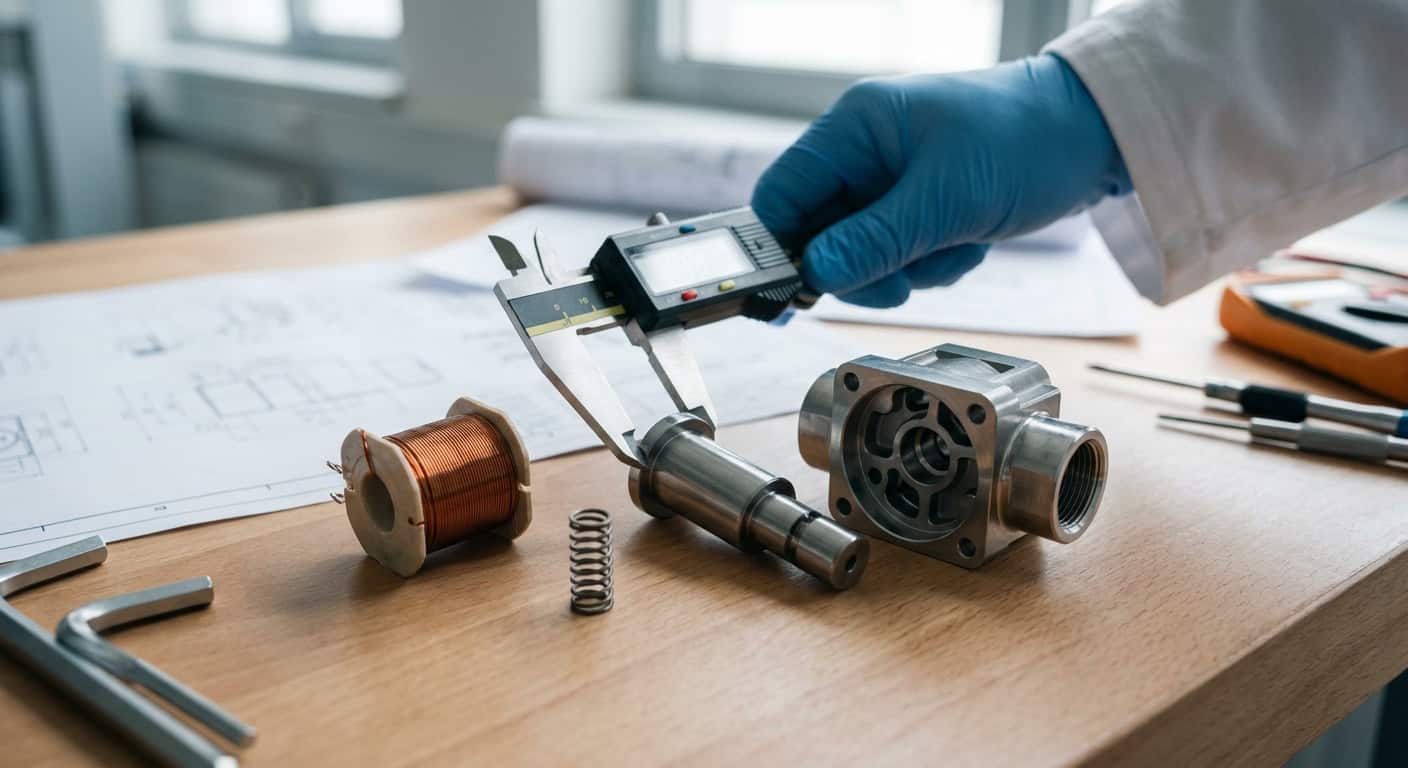
Contrary to intuition, the mechanical action of a solenoid valve is not determined solely by the current, but is governed by the magnetic circuit balance between the moving core and the stationary core. When the coil is energized, the generated electromagnetic force must overcome the spring’s pre-tension, the pressure differential resistance of the fluid medium, and the friction during the movement of the moving core to successfully complete the opening and closing actions.
The Pressure Differential Myth of Direct-Acting vs. Pilot-Operated Solenoid Valves
A 10% voltage fluctuation can cause the electromagnetic force to drop by nearly 20%, which is a physical detail most beginners overlook when calculating coil power consumption. Direct-acting solenoid valves rely directly on electromagnetic force to lift the valve plug, making them suitable for zero pressure differential or low-pressure environments. In contrast, pilot-operated solenoid valves rely on the medium’s own pressure differential to drive the main orifice. If the pressure differential between the system inlet and outlet is lower than the valve’s specified Minimum Operating Pressure Differential (MOPD), the valve will not open smoothly even if the coil is fully energized.
In the magnetic circuit design of solenoid valves, residual magnetism is not an inescapable physical curse, but rather an engineering variable that can be precisely predicted through material annealing processes and air gap control.
Undeniably, blindly choosing a high-power coil in the early design phase to pursue a safety factor often leads to severe temperature rise issues. When the viscosity of the solenoid valve’s operating medium exceeds 50 cSt, the chamfer tolerance of the standard moving core must be narrowed to within 0.02 mm; otherwise, fluid viscous drag will cause a response delay of over 150 milliseconds when starting at low temperatures.
Residual Magnetism and Spring Fatigue: The Physical Truth Behind Failure to Reset After De-energization
In a customized case for semiconductor cleaning equipment, the engineer overlooked the impact of medium viscosity on the moving core’s motion resistance, resulting in the valve failing to open at all under low temperatures. This was not a simple mechanical jam, but rather because the low temperature doubled the medium’s viscosity, offsetting the solenoid’s initial pull force.
How to Avoid Actuation Delay Caused by Solenoid Valve Residual Magnetism?
What cannot be seen on drawings is the fitting tolerance between the moving core and the armature tube, which directly determines the residual magnetism release speed and the valve’s response time. When the coil is de-energized, the magnetic field does not drop to zero instantly; the residual magnetic flux (residual magnetism) inside the magnetic material creates a continuous attraction force. If this attraction force is greater than the return spring’s push force, the moving core will experience a release delay or even fail to reset.
So, when a system faces high-frequency actuation demands, how do we balance response speed and coil lifespan? The solution is usually to design a non-magnetic air-gap spacer on the end face of the moving core or use high-purity electromagnetic soft iron materials to physically block the residual magnetic circuit.
Solenoid Valve Selection Metrics: A True Trade-off Between Power Consumption and Heat Generation
Compared to traditional single-voltage driving, adopting a dual-voltage (high startup voltage, low holding voltage) control circuit can increase actuation speed by 30% without increasing coil temperature rise. This control method applies a brief high voltage to the coil at the instant of startup to generate enough force to overcome static friction, and then drops to a holding voltage, significantly reducing power consumption during long-term energization.
The Impact of Duty Cycle on Solenoid Valve Lifespan
An actuation life of 3 million cycles is not achieved solely through material hardness; it depends even more on controlling the stress relaxation of the spring under long-term compression. For every 10°C rise in coil temperature, its insulation lifespan is roughly cut in half, making it critical to strictly evaluate the Duty Cycle during selection.
Frankly, no standard off-the-shelf solenoid valve can perfectly adapt to all extreme fluid environments, and customized magnetic circuits and seal structure designs are often uncompromising choices. When selecting a solenoid valve, the following key parameters must be included in the evaluation matrix:
- Medium viscosity and temperature variation range
- System minimum and maximum operating pressure differential (MOPD)
- Coil duty cycle and heat dissipation conditions
Solenoid Valve Procurement and Design Verification for High-Reliability Fluid Control Systems
When procurement personnel compare specification sheets, if they only focus on price and overlook the material differences in dynamic seals, they are highly prone to experiencing catastrophic medium leakage after a few months of operation. Fluororubber (FKM) and Ethylene Propylene Diene Monomer (EPDM) have fundamental differences in chemical resistance and temperature range; choosing the wrong material can cause the seals to swell or harden in specific media, thereby jamming the moving core.
The physical logic behind this tolerance is that when residual magnetism accumulates to a certain extent inside the valve body, if the spring’s return force is less than the residual magnetism attraction force, the valve will enter a “pseudo-energized” state where it cannot reset. In the field of fluid control, Shih Shin Technology, with its profound experience in electromagnetic simulation and materials engineering, helps clients avoid these hidden traps at the early design phase, providing precise customized magnetic circuit tuning services.
How can we ensure the consistency of residual magnetism and response time for each batch of solenoid valves in the global supply chain? The success of fluid control lies in the precise control of details. From magnetic circuit design to seal material selection, every step requires rigorous data support. Only through complete early-stage alignment of operating condition parameters and dynamic simulation can we ensure that the solenoid valve still actuates precisely after millions of cycles.
It is recommended during the early design stage to request from the supplier the electromagnetic force attenuation curve of the coil under the extreme operating temperature of 85°C, using it as a benchmark for the spring pre-tension design to ensure the reliability of resetting under long-term high-temperature operation.


